If you are looking for Cold Plate Manufacturers for AI servers, EV battery packs or power electronics, start with the ten below. Each one makes cold plates as a product line and discloses its capabilities publicly. The table shows where each fits, Step 3 narrows them to three or four to quote, and Step 6 lists the checks that remove suppliers before you commit.
- The ten manufacturers at a glance
- How the list was selected
- Step 1: Define your requirements
- Step 2: Choose the procurement mode
- Step 3: Shortlist by application scenario
- Step 4: Understand process differences
- Step 5: Full comparison of the ten manufacturers
- Step 6: Elimination criteria
- Step 7: Standards, cleanliness and filtration
- Step 8: Benchmark thermal and pressure-drop performance
- Step 9: Warranty and liability
- Step 10: Run every quote on the same test conditions
- Step 11: Plan lead time, MOQ and landed cost
- Documents to request before ordering
- Questions to ask suppliers
- FAQ
The ten manufacturers at a glance
Five key fields below. The full comparison, including founding year and main processes, is in Step 5.
| Company | Type | Location | Best for | Certification (per official site) |
|---|---|---|---|---|
| Jindu | Machining-based | Dongguan, China | Integrated heat sinks and liquid cold plates; custom CNC parts | IATF 16949 |
| Boyd | Comprehensive thermal management | USA | Aerospace, medical, data centers, EVs | ISO 9001, AS9100D, IATF 16949, ISO 13485, ISO 14001 |
| XD Thermal | Specialized liquid cooling (batteries) | Suzhou, China | EV battery packs, energy storage battery packs | IATF 16949 |
| CoolIT Systems | Specialized liquid cooling | Calgary, Canada | Server CPU/GPU direct-to-chip, OEM supply | ISO 9001, UL |
| Wakefield Thermal | Comprehensive thermal management | Nashua, New Hampshire, USA | Power modules, EV batteries | ISO 9001 (USA); ISO 9001, IATF 16949, ISO 14001 (China factory); ITAR |
| Motivair | Liquid cooling systems (including CDUs) | Lancaster, New York, USA | High-power CPU/GPU direct-to-chip | ISO 9001:2015; UL/CSA on cooling systems |
| ATS | Comprehensive thermal management | USA | Standard and custom parts; small batches and prototypes | ISO 9001:2015 |
| JetCool | Specialized liquid cooling | Littleton, Massachusetts, USA | Single-phase direct-to-chip, 350W to 3kW and above | UL certified (system-level) |
| Wieland MicroCool | Specialized cold plates | Pine Hall, North Carolina, USA | Power electronics, inverters, data centers, defense | Quality policy states AS9100D conformity |
| ToneCooling | Specialized cold plates | Boluo, Huizhou, Guangdong, China | GPU/CPU cold plates, IGBT, battery cold plates, energy storage | ISO 9001 |
How the list was selected
The list is not a ranking. Each company was included because its official website discloses cold plate products and at least one of the application areas in this guide. Market share, revenue and popularity were not used as selection criteria, because they are not reliable proxies for whether a supplier fits your design.
Eligible companies make cold plates as a product in their own right and supply them to server OEMs, system integrators, power electronics makers or battery pack builders. CoolIT Systems, Motivair and JetCool also sell CDUs or manifolds; only their cold plate offering is assessed here. Pure system vendors, such as large data center infrastructure companies and server OEMs that ship complete liquid-cooled racks, are not included. If you need a turnkey system, Step 2 explains when a bundled server purchase fits better than buying cold plates separately.
The ten companies fall into four groups:
- Global thermal manufacturers with broad portfolios: Boyd, Wakefield Thermal, ATS, Wieland MicroCool. Strong certification coverage, often less flexible for fast, highly customized AI loop changes.
- AI and direct-to-chip liquid cooling specialists: CoolIT Systems, Motivair, JetCool. Focused on high heat flux processors and CDU-based loops.
- Battery and EV specialists: XD Thermal, with an IATF 16949 scope for automotive and energy storage applications.
- Asian high-volume and custom manufacturers: Jindu, ToneCooling. Multiple processes (CNC, friction stir welding, brazing, embedded tube) and strong prototype flexibility.
Step 1: Define your requirements
Without these inputs, no supplier comparison has a basis. Write them down before you request quotes.
- Thermal load: heat output per device in watts, the heated area, and the resulting heat flux in W/cm²
- Coolant and interfaces: water, glycol solution or another coolant; target flow rate, allowable pressure drop and inlet temperature
- Mechanical envelope: footprint, mounting pattern, mounting pressure and flatness requirement, port type and location
- Volume and stage: prototype, small-batch validation, or stable mass production; annual demand and forecast growth
- Certification requirements: whether IATF 16949 (automotive), AS9100D (aerospace and defense) or ISO 13485 (medical) is mandatory, or whether ISO 9001 is enough
- Destination and compliance: country of installation, export controls, and any origin restrictions that affect supplier choice
Step 2: Choose the procurement mode
Decide whether the cold plate will be bought as part of a complete server or purchased separately. The choice determines who owns thermal performance, leak liability and warranty claims, and which suppliers you should contact.
Bundled with the server
Server OEMs integrate cold plates and manifolds at the factory. Thermal validation, warranty and service sit with one company. This suits buyers deploying accelerators at scale who do not want to own thermal design.
Purchased separately
You buy directly from a cold plate manufacturer and design or integrate the loop yourself. This suits integrators, retrofits and custom hardware. You must coordinate thermal performance, coolant flow and leak risk, and the warranty split must be written into the contract.
Whichever mode you choose, write down three things: who owns the thermal guarantee, who owns leak liability, and who is the single point of contact when a fault appears after integration. That answer will eliminate many suppliers immediately.
Step 3: Shortlist by application scenario
Use this table to narrow the ten companies to three or four to quote. It reflects capabilities each company discloses on its official site. It defines who to ask for quotes, not who is best.
| Your scenario | Shortlist to request quotes from | Basis (disclosed on official sites) |
|---|---|---|
| AI servers, direct-to-chip for CPU/GPU, OEM supply | CoolIT Systems, Motivair, JetCool, ToneCooling | CoolIT offers cold plates for NVIDIA and AMD platforms; Motivair says single-chip capacity can scale above 1000W; JetCool covers 350W to 3kW and above; ToneCooling offers cold plates for the GB200 platform (confirm current product scope with the supplier) |
| EV battery packs or energy storage battery packs | XD Thermal, ToneCooling, Wakefield Thermal | XD Thermal’s main products are battery liquid cold plates and it holds IATF 16949; ToneCooling has a battery cold plate line and states a typical prototype lead time of 4–6 weeks; Wakefield’s datasheet lists EV battery cooling applications |
| Power modules such as IGBT and SiC | Wakefield Thermal, ToneCooling, Wieland MicroCool | Wakefield’s datasheet lists compatibility with IGBT, SiC and GaN devices; ToneCooling has a dedicated IGBT cold plate page; Wieland products are used in inverters and DC-DC converters |
| Prototyping, small batches or standard parts | ATS, Jindu, ToneCooling | ATS has standard cold plate products available through distributors; Jindu is CNC-based and suits custom parts; ToneCooling states a typical prototype lead time of 4–6 weeks |
| Aerospace, defense, or US-made requirements | Boyd, Wieland MicroCool, Wakefield Thermal, Motivair | Boyd lists AS9100D on its site; Wieland’s quality policy states conformity with AS9100D; Wakefield holds ITAR registration; Motivair says its cold plates are made in the USA |
Step 4: Understand process differences
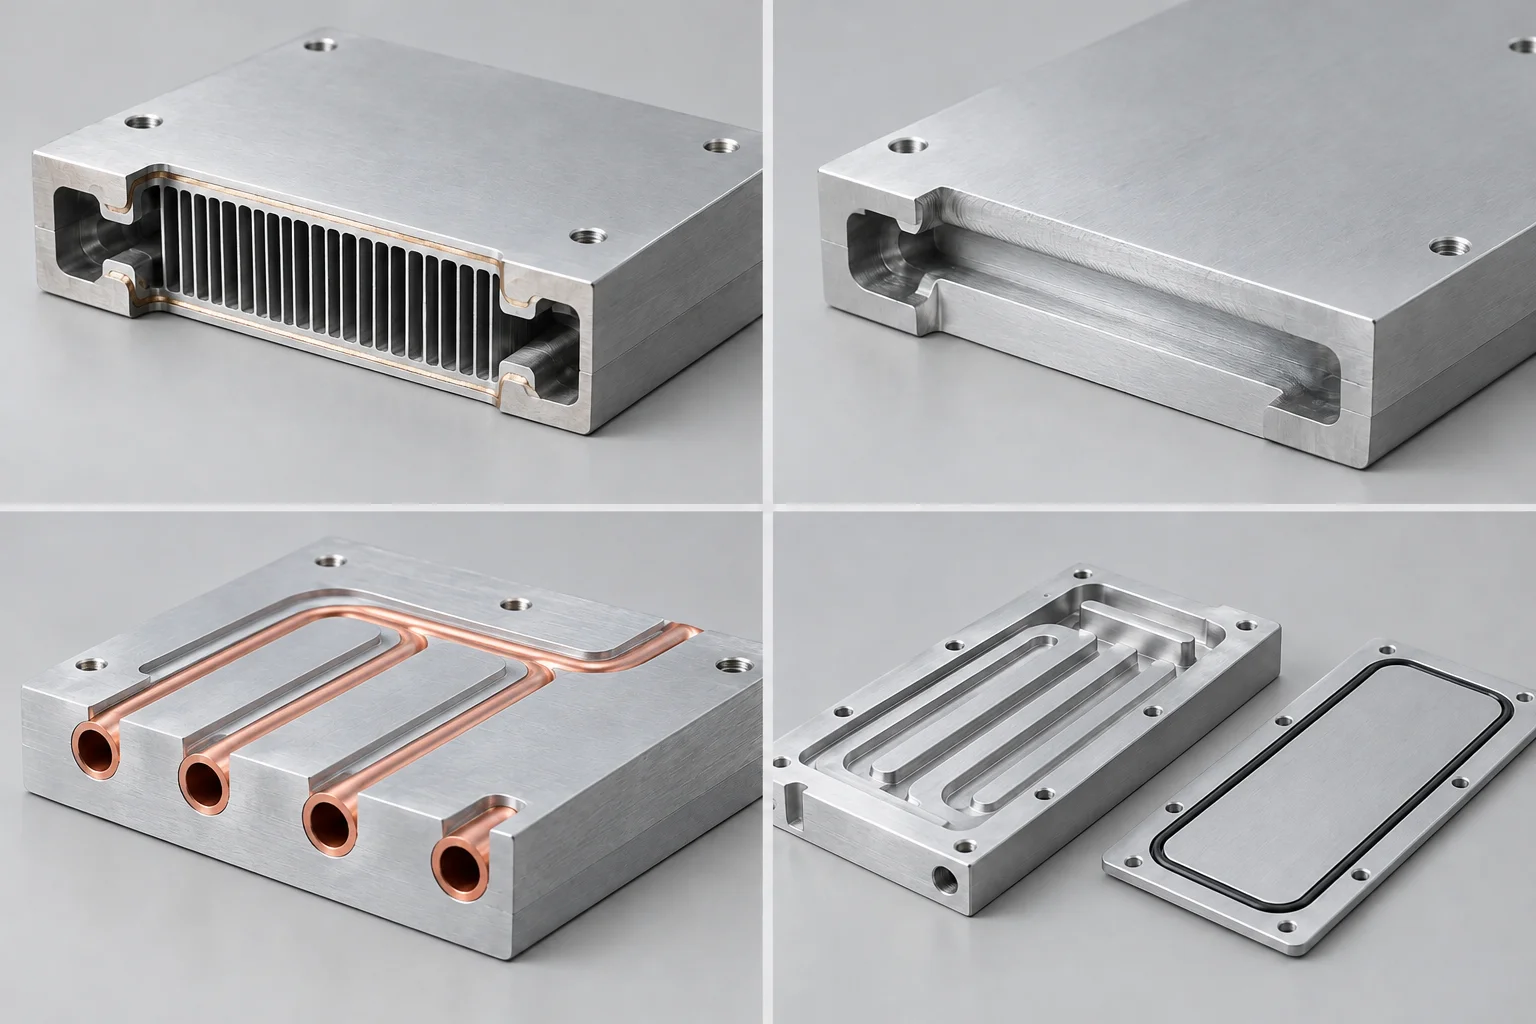
The same cold plate can perform differently in heat transfer, sealing and cost depending on how it is made. Process choice also affects what you must test. The table gives general characteristics; verify what each supplier actually runs.
| Process | Common materials | Design freedom | Sealing | Suitable for | Watch out for |
|---|---|---|---|---|---|
| Vacuum brazing | Aluminum, copper, copper–aluminum combinations | High; complex internal channels are achievable | Depends on process control; confirm leak testing piece by piece | High heat flux, complex channels | Joint quality depends heavily on fixture and process control; review leak-test records from production parts |
| Continuous (furnace) brazing | Aluminum, typically with clad brazing sheet | Medium; suited to repeatable flow geometries | Consistent across large batches when the process is controlled | High-volume production with stable designs | Higher tooling commitment; changes to channel geometry are costly |
| Friction stir welding (FSW) | Aluminum; copper–aluminum combinations | Medium to high | Solid-state joining without melting the base material | Demanding sealing requirements, lightweighting | Limited materials and thicknesses; confirm the supplier’s equipment capability |
| Embedded tube | Copper or aluminum tube pressed into a plate | Low; limited by tube bend radius | Depends on the number of sealed joints; more joints means more risk | Cost-sensitive industrial and telecom equipment | Confirm bend radius and joint positions against your layout |
| CNC machining (with cover) | Aluminum, copper | High; suits non-standard structures | Depends on how the cover is sealed; verify separately | Small batches, custom parts, precision fits | Higher unit cost; compare economics as volume grows |
| Skiving | Aluminum, copper | Medium; suits fin structures | Usually used for heat sinks and does not seal a flow channel | Fins for air-cooled or liquid-cooled heat sinks | Mostly heat sinks rather than cold plates; distinguish them when specifying |
Step 5: Full comparison of the ten manufacturers
This table expands the at-a-glance view. Read it as a starting point for due diligence. Every blank or “not published” cell is a question to put to the supplier when requesting a quote. A supplier that cannot fill a gap with verifiable evidence has told you something useful.
| Company | Company type | Location | Year founded | Suitable for | Main processes / products | Certifications (official site) |
|---|---|---|---|---|---|---|
| Jindu | Machining-based (CNC and thermal management) | Dongguan, Guangdong, China | 2012 | Integrated heat sinks and liquid cold plates; custom CNC parts | Skiving, FSW, brazing, CNC | IATF 16949 |
| Boyd | Comprehensive thermal management | USA | 1928 | Aerospace, medical, data centers, EVs | Liquid cold plates, two-phase cooling; states 100% leak testing of cold plates | ISO 9001, AS9100D, IATF 16949, ISO 13485, ISO 14001 |
| XD Thermal | Specialized liquid cooling (batteries) | Suzhou, Jiangsu, China | 2022 | EV battery packs, energy storage battery packs | Battery liquid cold plates, extruded liquid cooling tubes | IATF 16949 |
| CoolIT Systems | Specialized liquid cooling | Calgary, Canada | 2001 | Server CPU/GPU direct-to-chip, OEM supply | Cold plates, cold plate loops, rack manifolds, CDUs; production in Canada, Vietnam and China | ISO 9001, UL |
| Wakefield Thermal | Comprehensive thermal management | Nashua, New Hampshire, USA | 1957 | Power modules, EV batteries | Vacuum brazing, FSW, embedded-tube liquid cold plates | ISO 9001 (USA); ISO 9001, IATF 16949, ISO 14001 (China factory); ITAR |
| Motivair | Liquid cooling systems (including CDUs) | Lancaster, New York, USA | 1988 | High-power CPU/GPU direct-to-chip | Dynamic cold plates (proprietary design), rack manifolds, CDUs | ISO 9001:2015; UL/CSA on cooling systems |
| ATS | Comprehensive thermal management | USA | 1989 | Standard and custom parts; small batches and prototypes | Copper-tube cold plates, stainless-tube cold plates, custom cold plates, double-sided cold plates | ISO 9001:2015 |
| JetCool | Specialized liquid cooling | Littleton, Massachusetts, USA | 2019 | Single-phase direct-to-chip, 350W to 3kW and above | Micro-jet and microchannel cold plates; CDUs, manifolds | UL certified (system-level) |
| Wieland MicroCool | Specialized cold plates | Pine Hall, North Carolina, USA | 2019 | Power electronics, inverters, data centers, defense | FSW single-phase cold plates; patented micro-deformation technology (MDT) | Quality policy states AS9100D conformity |
| ToneCooling | Specialized cold plates | Boluo, Huizhou, Guangdong, China | 2004 | GPU/CPU cold plates, IGBT, battery cold plates, energy storage | CNC, FSW, vacuum brazing, embedded tube | ISO 9001 |
Boyd ownership: Boyd Thermal was reported in March 2026 to have been acquired by Eaton. Confirm current ownership and the contracting entity before ordering.
Step 6: Elimination criteria
These five criteria are pass/fail. If a supplier fails one, remove it from the shortlist and spend your time on the survivors rather than keeping it “to be fair.”
1. Process coverage: can they recommend a process for your application?
A supplier that offers only one process will tend to recommend it. A supplier that offers brazing, FSW and embedded-tube options, and can explain the trade-offs in heat flux and channel geometry, shows real selection capability.
2. Verification capability: leak testing and thermal testing
Ask what leak-test method is used, at what test pressure, against what leak-rate criterion, and whether every part is tested. Ask whether thermal and pressure-drop testing is done on production parts. These are direct evidence of production control.

3. Certification authenticity: can the certificates be verified?
For each certification on the supplier’s site, obtain the certificate and check the certificate number, issuing body, scope and validity period against the certification body’s public database. Certification mentioned only in marketing copy does not count.
4. Capacity and delivery: evidence from production, not samples
Ask for production line scale, inspection records from production lots, realistic prototype and production lead times, and minimum order quantities. If the only data offered comes from samples, request more.
5. Comparable projects: experience close to your requirements
Ask for at least one reference case close to your power level, volume and application, and for a contact you can speak with. Without a comparable case, production experience on your type of hardware is unproven.
Example of a reference claim to verify
Boyd states publicly that it has delivered 5 million liquid cold plates to hyperscale customers and that its cold plates are 100% leak tested after machining and brazing. These are company statements from a 2025 press release. Treat them as claims to test, not facts: ask for a named reference or a contact who can confirm volume and test coverage for a product close to yours.
Step 7: Standards, cleanliness and filtration
Many cold plate failures are not caused by the plate design. They come from contamination, corrosion, pump or filtration mismatch, and test conditions that do not match the installed system. Before approving a supplier, confirm how they address each of the following.
- Standards the supplier tests to: ask which standards govern the supplier’s leak testing, pressure testing and environmental testing. Relevant references include ASHRAE liquid cooling guidance on supply temperature and facility conditions, IEC environmental test methods for thermal cycling, humidity and vibration, and leak-test methodology standards such as EN 1779 for pressure and leak testing. Confirm the supplier’s actual procedure rather than accepting a standard name alone.
- Internal cleanliness: ask what cleanliness level the supplier guarantees before shipping, how it is measured, and whether residue from machining, brazing flux or cleaning is checked.
- Filtration compatibility: ask what filter rating the supplier recommends for its channel geometry. Microchannels are particularly sensitive to particles and bubbles; a filter specification should be part of the system design, not an afterthought.
- Coolant and material compatibility: ask for corrosion test results for the specific material pairing and coolant chemistry you will run, including inhibitor type and concentration.
Step 8: Benchmark thermal and pressure-drop performance
Thermal resistance tells you how effectively heat moves from the heated surface to the coolant. It is calculated as Rth = ΔT / Q, where ΔT is the temperature difference between the heated surface and the coolant and Q is the heat load in watts. Rth is measured in K/W. A low number is only meaningful if the test conditions match your application.
When you compare suppliers, insist on the following:
- Test conditions stated in full: heat load, heated area, coolant type, flow rate, inlet temperature, mounting pressure, contact surface and interface material.
- Temperature maps, not a single number: a single average can hide hot spots, especially where the processor package is not flat.
- Pressure-drop curves at several flow rates: a plate that meets the thermal target may consume more pump head than your system can supply.
- Statistical process data: for production lots, ask for process capability data (such as CPK) on critical dimensions and batch distributions of pressure drop and thermal resistance.
Verify one number yourself. Before a bulk order, run a pressure-drop check on a sample: pump, flow meter and pressure gauges at inlet and outlet, at your actual flow rate. If the measured pressure drop is materially higher than the quoted value, a gap of 20% or more is a reasonable trigger for questions. Ask the supplier to explain the discrepancy before scaling. A supplier that can explain the gap is worth keeping. One that cannot has shown how much its other numbers are worth.
Worked example: pressure-drop check (illustrative numbers)
Quoted pressure drop: 5.0 kPa at 2.0 L/min. Measured on your test loop at the same flow: 6.2 kPa. The gap is (6.2 − 5.0) / 5.0 = 24%, which passes the 20% trigger. Before concluding the supplier is wrong, check your own test setup: fitting and tubing losses, coolant temperature and viscosity, and whether the sample matches production geometry. Then ask the supplier to explain the remaining difference.
Worked example: channel depth capability (illustrative numbers)
Specification: channel depth 1.00 mm ± 0.05 mm, so USL = 1.05 mm and LSL = 0.95 mm. Production lot mean μ = 1.01 mm, standard deviation σ = 0.012 mm. Cpk = min(USL − μ, μ − LSL) / 3σ = min(0.04, 0.06) / 0.036 ≈ 1.11. A Cpk of 1.11 means the process is capable in this example, but the mean sits off-center toward the upper limit. Ask the supplier why, and confirm the Cpk your own quality system requires; 1.33 is a common benchmark in many industries.
Step 9: Warranty and liability
Who pays when a cold plate fails is usually decided at order placement. The contract should cover at least the following:
- Basis for thermal guarantees: the operating conditions under which thermal resistance and pressure drop are guaranteed, and whether they match your actual use.
- Leak liability period: how long the warranty lasts, and whether it covers the plate body only or also fittings, manifolds and joints.
- Responsibility boundaries: who is responsible for the cold plate, manifold, CDU and server, and how faults are divided after integration.
- Remedy for batch defects: whether a batch-wide defect results in replacement, rework or compensation, and who pays for removal and reinstallation.
- On-site support: the scope of technical support during installation and commissioning, and whether it is charged.
Step 10: Run every quote on the same test conditions
When you send an RFQ, give every supplier the same conditions. If each supplier tests under different assumptions, their thermal resistance and pressure-drop numbers cannot be compared. Specify:
- The same heat load and heated area
- The same coolant type, concentration and flow rate
- The same inlet temperature and target contact-surface temperature
- The same contact-surface size, mounting method and mounting pressure
Ask each supplier to state which of these conditions its published data uses, and to retest under yours if they differ.
Step 11: Plan lead time, MOQ and landed cost
Ranges below are indicative planning figures for RFQs, not supplier commitments or verified quotations. Actual values depend on design, material, testing, volume and destination. Use them to sanity-check quotes, then get written confirmation from each supplier.
| Supplier profile | Typical construction | Indicative MOQ for a new design | Indicative lead time | Main cost drivers |
|---|---|---|---|---|
| Prototype and engineering-focused shop | CNC-machined copper or aluminum; drilled or milled channels; sealed or brazed cover | About 1–20 units | About 2–6 weeks after drawing approval; complex designs take longer | Engineering time, fixtures, inspection, prototype shipping |
| Production CNC and brazing supplier | Machined plate with brazed cover; copper or aluminum depending on thermal, weight and corrosion needs | About 50–500 units; first order may carry setup cost | About 4–10 weeks for first production; repeat orders can differ | Machining time, braze yield, post-processing, inspection level |
| High-volume formed or stamped supplier | Formed or stamped plates joined by a validated process | Often 1,000+ units; dedicated tooling may be needed | About 8–16 weeks or more including tooling and qualification | Tooling amortization, minimum order commitments, scrap assumptions, inventory carrying cost |
| Automotive-oriented supplier | Application-specific brazed, welded or machined assemblies | Program-dependent; usually well above prototype quantities | Add supplier qualification and product validation to manufacturing lead time | Validation, documentation, audits, traceability, warranty exposure |
| Regulated or high-reliability supplier | Design and process set by the operating environment and buyer requirements | Set by qualification scope rather than a universal MOQ | Qualification and documentation extend the schedule; use milestone-based delivery | Qualification builds, special inspection, controlled packaging, customer audits |
Compare landed cost, not unit price. Total cost should include unit price, tooling, testing, packaging, freight, duties and taxes, quality costs (rework, scrap, returns), inventory and payment terms. The lowest unit price can hide poor flatness or inconsistent channel depth, which show up later as cost.
Build a schedule buffer. Sample lead times rarely repeat exactly in production, and tooling or fixture changes can add weeks.
Documents to request before ordering
- Certificates: scanned copies, checked against certificate number, issuing body, scope and validity period, and confirmed to cover the factory making your parts
- Leak-test reports: test method, test pressure, leak-rate criteria, and confirmation that every part is tested
- Production-part test data: thermal resistance and pressure-drop data from parts drawn from production, not only samples
- Statistical process data: process capability on critical dimensions and batch distributions for pressure drop and thermal resistance
- Thermal simulation report: based on your operating conditions, not a generic template
- Reference cases: at least one case close to your application, power level and volume
- Coolant and material compatibility data: corrosion test results for your material pairing and coolant chemistry
- Material certificates: mill certificates for the aluminum or copper grade used, traceable to production lots
- Written warranty terms: scope, duration and responsibility boundaries
Questions to ask suppliers
| Question | Why ask |
|---|---|
| Can you provide test data from production parts, not only samples? | Sample and production performance can differ; production data reflects the real level |
| What leak-test method do you use, at what pressure and leak-rate criterion? Is every part tested? | Leakage is a common failure mode; per-part testing is more reliable than sampling |
| Which process would you recommend for our heat flux and channel geometry, and why? | Shows whether the supplier selects processes or only sells what its equipment makes |
| What cleanliness level do you guarantee before shipping, and how is it measured? | Contamination is a frequent cause of pressure-drop rise and flow maldistribution |
| What filtration do you recommend for this design? | Confirms the supplier has considered the system, not only the plate |
| What process capability data (such as CPK) do you have on critical dimensions? | Shows whether production is controlled, not only inspected |
| Can you provide the latest certificate with number, issuing body, scope and validity period? | Prevents certification existing only as a claim on the website |
| Can you provide mill certificates traceable to our production lot? | Confirms the material grade actually used |
| Under what conditions were thermal and pressure-drop data measured? Can you retest under ours? | Data from different conditions cannot be compared |
| Have you tested our coolant and material combination for corrosion? | Corrosion develops slowly and is hard to detect in short tests |
| What do the warranty and leak liability cover, and for how long? | Unclear responsibility can make losses far exceed the cost of the plate |
| What are the MOQ, sample lead time and production lead time, and what drives them? | These set schedule and upfront cost |
| What are the total landed costs, including duties, freight and any tooling? | Unit price alone does not reflect what you will pay |
| Do you have production reference cases close to our application? Can we speak with a contact? | Verifies performance on comparable projects |
FAQ
Are cold plate manufacturers the same as liquid cooling system vendors?
No. Cold plate manufacturers make the plate that contacts the processor. System vendors sell complete liquid-cooled servers, racks, CDUs and manifolds, and may or may not make their own plates. Step 2 explains how to decide between buying a bundled system and buying cold plates separately.
How do I verify a supplier’s certifications?
Request scanned copies, check the certificate number, issuing body, scope and validity period, and look them up in the certification body’s public database. A certificate download on the supplier’s website is a reference, not a verification. Confirm the certificate covers the specific factory making your parts.
If the samples pass, will mass production pass?
Not necessarily. Process variation between samples and production runs can change thermal and leak results. Require test data from production parts before ordering, and ask for process capability data on critical dimensions.
How do I assess leak risk?
Ask for the leak-test method, test pressure and acceptance criterion, request inspection records, and confirm whether every part is tested. Per-part testing is more reliable than sampling. Also ask how the supplier handles pressure cycling and whether its testing covers the joints and fittings you will use.
Should I buy bundled with the server or purchase cold plates separately?
If you are a system integrator or need to deploy accelerators quickly, bundled procurement keeps thermal performance and warranty with one company. If you are designing your own loop or retrofitting an existing system, separate purchasing is more flexible, but you take on thermal and leak coordination yourself.
How many suppliers should I quote?
Three or four is usually enough to compare meaningfully. Quote suppliers that pass the scenario shortlist in Step 3, and send all of them the same conditions from Step 10. More quotes than that rarely improve the decision and add comparison effort.
How should I think about tariffs and export controls?
Duties, freight, origin rules and export controls can change the total cost and the eligible supplier list. Confirm the destination, the applicable duty treatment and any export restrictions with your customs broker or trade advisor before finalizing the supplier, because the answer depends on product classification and the rules in force at the time of import.
