As electronic devices become more powerful and component heat flux increases, removing heat through air alone becomes increasingly difficult. Air cooling relies on moving air across a heat sink or other heat-transfer surface. Its effectiveness depends on available surface area, airflow, ambient temperature, and the thermal resistance between the heat source and the surrounding air. When a component generates more heat than the air-cooling system can dissipate within its temperature limits, simply increasing fan speed may introduce excessive noise, power consumption, space requirements, or diminishing thermal returns. Liquid cooling addresses this constraint by changing the heat-transfer path: instead of relying entirely on air moving across the component, a liquid cold plate transfers heat into a circulating coolant that carries it to a remote heat exchanger.
A cold plate is the starting point of this liquid-cooling thermal path. Heat travels from the electronic device through a thermal interface material (TIM), into the cold plate base, across the internal channel walls, and into the coolant. The heated coolant then moves through the loop to a radiator, chiller, or other heat exchanger, where the heat is rejected elsewhere. The performance of this entire path depends on the interfaces and components working together. A highly conductive plate cannot compensate for poor TIM contact, inadequate coolant flow, excessive pressure drop, or an undersized heat exchanger.
At Jindu, we manufacture the component where conduction meets convection — using skiving, friction stir welding (FSW), vacuum brazing, soldering, and precision CNC machining, with 100% air-tightness validation before shipment. These manufacturing processes support different cold plate geometries, sealing requirements, and thermal design objectives. For product-level details and manufacturing options, explore our liquid cold plate manufacturing capabilities.
Cold Plate Definition and the Synonyms You Will Encounter
A cold plate is a heat-transfer component designed to remove heat from a device through direct thermal contact and transfer that heat to a cooling medium, commonly a liquid flowing through internal channels. Its main elements typically include a thermal contact surface, a conductive base, internal flow passages, and a sealed structure that keeps the coolant contained. Heat passes from the source into the plate by conduction and then from the internal channel surfaces into the flowing coolant by convection. Cold plates are used in applications where concentrated heat loads, temperature uniformity, or limited installation space make conventional air cooling insufficient. The terms cold plate, liquid cold plate, coldplate, water cooling plate, and liquid cooling plate are often used to describe this general component category.
Actual designs differ in material, channel architecture, joining process, pressure capability, and mounting interface. Learn more about the available designs from our liquid cold plate manufacturer page.
How Does a Cold Plate Work? Conduction, Convection, and the System Around It
The Two-Step Thermal Path
A cold plate transfers heat through two primary mechanisms: conduction through solid materials and convection between the internal channel surfaces and the coolant. Both stages must be considered when evaluating thermal performance.
Step 1: Conduction from the heat source into the plate. Heat first travels through the component package and thermal interface material before entering the cold plate base. TIM thickness, contact pressure, surface condition, and base flatness all influence the resistance of this interface. A thicker TIM layer generally introduces additional thermal resistance, while insufficient clamping pressure can leave microscopic air gaps between surfaces. Excessive pressure, however, may damage the component or distort the plate. The contact surface must therefore match the mounting requirements and mechanical limits of the application.
Flatness should not be treated as a single measurement taken only after manufacturing. A cold plate that is flat at shipment but bows under thermal cycling accelerates TIM pump-out; flatness stability, not just initial flatness, is a specification variable. Repeated temperature changes and mechanical loading can alter the contact interface over time, reducing the consistency of heat transfer even when the original dimensions met the drawing requirements.
Step 2: Convection from the channel walls into the coolant. Once heat reaches the internal channel surfaces, the flowing coolant absorbs it and transports it through the cooling loop. Wetted area, channel geometry, coolant properties, flow rate, and flow regime affect the rate of heat transfer. Increasing surface area or promoting mixing can improve convection, but these changes may also increase pressure drop. The design objective is not simply to maximize channel complexity; it is to achieve the required thermal resistance within the available pumping capacity and system pressure limits.
In practical terms, conduction performance is strongly influenced by interface quality, TIM thickness, mounting pressure, and plate geometry. Convection performance depends on the relationship between wetted area, flow distribution, coolant properties, and pressure drop. Thermal simulation and testing help determine whether the combined design meets the application’s temperature limits.
Why the Cold Plate Cannot Be Evaluated in Isolation
A cold plate operates as part of a closed-loop cooling system, not as an independent heat-removal device. The pump determines the available flow and pressure, while manifolds distribute coolant among parallel branches. A coolant distribution unit (CDU) manages the interface between the cooling loop and the wider facility or equipment system. Filtration protects the passages against particles and manufacturing residues, and the remote heat exchanger determines how effectively the coolant can release the absorbed heat.
If the manifold distributes flow unevenly, some cold plates may receive less coolant than intended. If the pump cannot overcome the combined pressure drop of the plates, piping, valves, and fittings, the actual flow may fall below the design target. Inadequate filtration can gradually restrict channels, while insufficient heat-exchanger capacity can cause coolant inlet temperatures to rise. Each condition can reduce performance even when the cold plate itself has been manufactured correctly.
This is why we validate air-tightness and support thermal simulation and heat-dissipation analysis alongside the mechanical design. The cold plate’s operating conditions, coolant requirements, interface geometry, and pressure limits should be considered together with the surrounding system.
Cold Plate Types and Internal Channel Architectures
Before choosing a type, understand that the cold plate’s thermal face is an interface, not a perfect plane — the target chip’s integrated heat spreader (IHS) profile matters as much as the plate’s own flatness. The best architecture depends on heat flux, required thermal resistance, coolant pressure, manufacturing volume, sealing requirements, and the available installation space. A design that works well for a cost-sensitive industrial assembly may not provide the thermal performance or reliability needed for a high-heat-flux processor. Manufacturing method and final surface geometry must be considered together rather than selected independently.
Tubed Cold Plates
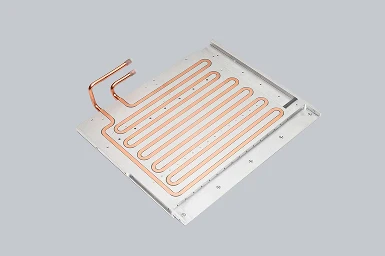
A tubed cold plate uses a tube as the coolant passage, with the tube attached to or embedded in a conductive body that provides the thermal contact surface. The tube carries coolant through a defined route while the surrounding body spreads heat from the component toward the tube wall. This architecture can be suitable for low-to-moderate power applications in which cost, straightforward construction, and relatively simple channel routing are important considerations.
Tube-based designs are typically soldered or mechanically pressed into a machined aluminum body. The thermal performance depends on the tube material, contact between the tube and body, available heat-transfer area, and coolant flow. The joining or retention method must maintain adequate contact and mechanical stability under the intended operating conditions. For applications with modest heat loads and less demanding thermal resistance targets, a tubed design may provide a practical balance between manufacturing complexity and cooling performance.
Machined Channel Cold Plates with Sealed Cover
A machined-channel cold plate is produced by cutting coolant passages directly into a metal base, commonly using CNC milling, and then sealing the open channels with a cover. The resulting geometry can accommodate specific inlet and outlet locations, flow paths, mounting features, and internal passage dimensions. Because the channels are formed in the base, designers can tailor the passage layout to the heat source and the available space.
The cover-joining method affects pressure capability, manufacturing cost, distortion, and long-term sealing reliability. Friction stir welding (FSW) can be suitable when a robust aluminum joint and reliable sealing are priorities, including designs with demanding pressure requirements. Vacuum brazing is useful when fins, covers, or other features require broad metallurgical bonding across multiple contact areas. The choice depends on the alloy, joint geometry, thermal cycle, and required finished dimensions.
Machined channels also introduce manufacturing considerations that should be addressed on the drawing. Channel depth, wall thickness, tool access, burr removal, sealing-land geometry, and post-joining machining allowances can all affect the final component. The design should leave sufficient material for finishing operations where the joining process may change the thermal contact surface.
Skived Fin Cold Plates
A skived fin cold plate uses a cutting process to lift thin fins from a solid metal base without cutting them completely away from the original material. The fins and base remain a continuous piece of metal, avoiding the additional interface resistance associated with separately attached fins. Skiving can produce high fin density and substantial surface area in a compact structure, making it useful for high-heat-flux applications where the internal geometry must provide effective heat transfer.
Because the fins are formed from the base material itself, the design does not introduce a separate fin-to-base brazed joint. This can be advantageous when minimizing interface resistance is important or when the application requires dense heat-transfer features. Fin height, thickness, spacing, material properties, and coolant flow still determine the final performance. High fin density alone does not guarantee better cooling if the geometry creates excessive pressure drop or poor flow distribution.
For applications that benefit from integral fin structures, see our skived fin cold plates. Jindu’s skiving capability supports the manufacture of compact thermal structures in which fin geometry and base construction must work together.
Vacuum Brazed Cold Plates
Vacuum brazed cold plates use a controlled brazing process to join fins, covers, or other metal features into a sealed assembly. The process can create broad metallurgical bonds across complex contact areas, allowing manufacturers to produce internal structures that would be difficult to make as a single machined component. Vacuum brazing is particularly relevant when the design requires multiple joined features and a compact arrangement of coolant passages or heat-transfer surfaces.
However, the brazing thermal cycle can change the shape of the plate. The thermal cycle moves the face — post-braze machining stock and a final leak test after the finish cut are not optional when the design requires tight contact-surface control and verified sealing. A design that allows no material for corrective machining may not retain the required flatness after joining. The manufacturing plan should therefore account for distortion, provide appropriate finishing allowances, and establish inspection criteria for the completed assembly.
Leak testing must be performed after the final machining operation that could affect a sealing boundary or coolant passage. Testing an unfinished assembly does not establish that the final component remains leak-tight after subsequent processing. Jindu performs 100% air-tightness testing before shipment according to the applicable product requirements. Learn more about our vacuum brazed cold plates.
FSW (Friction Stir Welding) Cold Plates
Friction stir welding joins metal components through frictional heating and mechanical stirring rather than conventional fusion welding. In aluminum cold plate manufacturing, FSW can create a solid-state joint between a machined base and a cover, supporting a sealed internal coolant structure. It is useful when the design requires a robust joint and when the material, geometry, and process parameters are compatible with friction stir welding.
FSW heats the aluminum locally to approximately 400–550°C in the process conditions described here; the face will move. Design with approximately 1 mm of post-weld machining stock where the geometry and distortion allowance require it, finish the contact surface after joining, and leak-test after the final cut — not before. The actual machining allowance should be confirmed through material selection, joint geometry, process development, and dimensional validation rather than applied as an unconditional value to every design.
The order of operations matters. Welding can introduce dimensional changes that affect the thermal contact face, mounting datums, and sealing geometry. Post-weld machining establishes the final interface, while subsequent leak testing verifies the completed coolant boundary. For designs that require this joining method, explore our friction stir welded cold plates.
Additive Manufactured / Conformal Cooling Cold Plates
Additive manufacturing can produce internal passages and conformal cooling geometries that are difficult to create using conventional machining or joining methods. It may be useful when highly customized internal flow paths or complex three-dimensional structures are required. However, material availability, internal surface quality, powder removal, inspection access, cost, and production repeatability must be evaluated for the specific application. Conventional skiving, CNC machining, FSW, and vacuum brazing remain relevant where their established manufacturing routes meet the required thermal, mechanical, and production targets.
Materials: Copper vs. Aluminum, and What Else Enters the Decision
Copper and aluminum are common cold plate materials, but neither is automatically the best choice for every design. Selection should account for thermal conductivity, total component weight, material cost, corrosion behavior, machinability, joining compatibility, and the required channel architecture. The material that offers the highest thermal conductivity may not produce the best overall solution if it increases mass, complicates manufacturing, or creates compatibility problems in the cooling loop.
Copper offers high thermal conductivity and can be attractive when rapid heat spreading is a major priority. It is often considered for compact heat-transfer structures or applications where the thermal resistance budget is particularly demanding. Its disadvantages can include higher material cost, greater weight, and more challenging machining and joining requirements. Copper also needs to be evaluated against the coolant chemistry and any dissimilar metals present in the system.
Aluminum offers a useful combination of low weight, thermal performance, machinability, and manufacturing flexibility. It is widely used in cold plate bodies, machined channels, skived fin structures, and joined assemblies. Aluminum can be more forgiving for FSW and brazing process development, depending on the alloy and joint configuration. Its corrosion behavior must nevertheless be considered carefully when the cooling loop contains copper or other dissimilar metals.
Copper is harder to machine and weld; aluminum is more forgiving for FSW and brazing — material and process must be decided together. Jindu’s CNC machining experience with copper and aluminum supports the evaluation of material choice alongside the required joining process, channel geometry, and final dimensional tolerances. The appropriate manufacturing route should be selected before the design is finalized, not after the material has been specified.
Other Material and Integration Options
Other material and integration options may be appropriate in particular applications:
- Stainless steel: May be considered where corrosion resistance, chemical compatibility, or mechanical requirements justify its use, although its thermal conductivity is generally lower than that of copper or aluminum.
- Nickel-plated surfaces: A nickel coating may be used to modify surface behavior or improve compatibility for a defined application. Coating integrity, coolant chemistry, and the potential for coating damage must be evaluated.
- Carbon-graphite: Selected carbon-based materials can support specialized heat-spreading or thermal-management functions, depending on their structure and integration requirements.
- Vapor chamber integration: A vapor chamber may be incorporated into a broader thermal design to spread concentrated heat before it enters the cold plate. Its value depends on the heat-source geometry, interface resistance, and system constraints.
The final material decision should therefore be based on the entire thermal and mechanical design, including coolant compatibility, manufacturing feasibility, joining requirements, and the expected operating environment.
Coolants and Compatibility: Water, Glycol, Deionized Water, and Dielectric Fluids
The coolant determines more than how heat is carried away. Its chemistry, electrical properties, viscosity, additives, and interaction with wetted materials affect corrosion risk, pressure drop, maintenance requirements, and long-term channel cleanliness. Water and water-glycol mixtures are common choices for liquid-cooling loops, while deionized water and dielectric fluids may be used in more specific system designs. No coolant should be selected solely on the basis of thermal conductivity without checking its compatibility with the complete wetted-material system.
The following table is a preliminary screening guide rather than a universal compatibility certification. Actual compatibility depends on alloy grade, coolant formulation, inhibitor package, temperature, electrical conditions, seals, coatings, and operating duration.
| Wetted material | Water | Glycol-water mixture | Deionized water | Dielectric fluids: PAO, silicone, fluorinated fluids |
|---|---|---|---|---|
| Copper | Potentially suitable with controlled chemistry and appropriate corrosion management. | Depends on the glycol formulation, inhibitors, temperature, and mixed-metal loop. | Requires monitoring because water chemistry and conductivity can change during operation. | Depends on the specific fluid, seals, coatings, and component materials. |
| Aluminum | Requires control of pH, dissolved species, and corrosion inhibitors where applicable. | Requires a compatible inhibitor package and careful control in mixed-metal systems. | Requires a validated chemistry and monitoring plan; deionized does not mean corrosion-proof. | Requires fluid-specific compatibility testing, including seals and surface treatments. |
| Stainless steel | Often suitable, depending on grade, water chemistry, and chloride exposure. | Depends on the fluid formulation, temperature, and other loop materials. | Requires consideration of grade, operating chemistry, and system contamination. | Depends on fluid formulation, seals, and the full wetted-material assembly. |
Glycol can help provide freeze protection and other operating benefits, but it does not automatically eliminate corrosion risk. In a mixed copper-aluminum loop, dissimilar-metal contact, coolant chemistry, inhibitor depletion, and electrical conditions can contribute to galvanic corrosion. The complete loop should be designed around compatible materials and a coolant specifically formulated for the intended service.
Filtration is equally important. Particles and residues can accumulate in narrow channels, reducing the available flow area and changing pressure drop. A filtration specification should therefore reflect the smallest relevant channel feature, the coolant cleanliness requirement, and the contamination risks introduced during manufacturing, assembly, and maintenance.
Early Warning Signs of Galvanic Corrosion — What to Monitor Before the Leak
Galvanic corrosion can progress before an obvious external leak appears. Monitoring coolant condition and hydraulic performance can help identify developing problems, although no single indicator proves that galvanic corrosion is occurring. A useful monitoring plan establishes a baseline after commissioning and tracks changes under comparable operating conditions.
- Rising coolant electrical conductivity: An increase may indicate that dissolved ionic species or contamination are accumulating. Interpret the trend alongside coolant type, temperature, and the system’s established baseline.
- pH drift: A sustained shift away from the coolant supplier’s specified range may indicate chemical degradation, contamination, or changes in inhibitor performance.
- White or blue-green gel-like deposits: Deposits may indicate corrosion products or coolant degradation, but their composition should be confirmed before drawing a conclusion.
- A gradually increasing inlet-to-outlet temperature difference: Under comparable heat loads and flow conditions, a changing temperature difference may indicate reduced flow, fouling, or a change in heat-transfer performance.
- Aluminum ion concentration above 1 ppm: This can be treated as a screening trigger for investigation when appropriate to the coolant chemistry and measurement method. It is not a universal failure threshold; confirm the result and compare it with the applicable coolant specification and baseline.
- An unexplained rise in pressure drop: A rising pressure drop at comparable flow conditions may indicate channel restriction, deposits, or other hydraulic changes. Check instrumentation and operating conditions before attributing the change to corrosion.
Surface treatment such as anodizing slows galvanic attack, but it cannot replace loop-level monitoring — cold plate life is co-determined by plate chemistry and loop chemistry. Anodizing and sandblasting may be available as manufacturing surface treatments, but their suitability depends on the application. Anodizing must be specified with attention to coating integrity and the areas that require electrical, thermal, or sealing contact. Surface treatment should complement, rather than replace, coolant compatibility controls, inspection, and maintenance.
Channel Cleanliness Is a Manufacturing CTQ, Not a System Afterthought
Microchannel blockage can originate from manufacturing residues as well as from coolant degradation products. Metal chips, burrs, brazing flux residues, and particles introduced during assembly can remain inside a passage if cleaning and verification are inadequate. Once the system is operating, such contaminants may migrate, accumulate in narrow sections, obstruct local flow, or contribute to changes in pressure drop. External dust is not the only concern, and it is often not the primary source of contamination inside a sealed liquid-cooling circuit.
Channel cleanliness should be defined as a critical-to-quality (CTQ) requirement and controlled through the manufacturing process. After CNC machining, the process should address burr removal, chip evacuation, flushing, drying, and cleanliness verification. The inspection method and acceptance criteria should be appropriate to the internal geometry and the intended coolant. For brazed structures, the cleaning and verification plan should also account for the joining process and any residues that may remain after thermal processing.
Filtration should be selected in relation to the smallest relevant channel feature and the system’s contamination tolerance. A filtration range of 25–50 μm can serve as an initial reference for some microchannel applications, but it is not a universal specification. The appropriate filter rating depends on the minimum passage dimensions, particle-size distribution, allowable pressure drop, filter capacity, and the risk of particles obstructing critical features.
Jindu connects CNC finishing and post-processing with explicit cleanliness requirements — deburring, flushing, drying, and verification — as part of the manufacturing plan. A drawing or quality plan that specifies only channel dimensions without defining cleanliness leaves a critical part of the manufacturing requirement open to interpretation.
Where Cold Plates Are Used: Applications and What Each Application Demands
AI Servers and Data Center Liquid Cooling
AI computing platforms are increasing the heat-removal demands placed on data center infrastructure. The GB300 platform has been associated with rack-level power requirements above 140 kW, while some reported configurations assign approximately 85–90% of compute-tray heat removal to liquid cooling. GPU thermal design power has also moved from the 700 W class toward the 1,400 W class in high-performance configurations. These figures describe specific platform contexts rather than universal values for every rack or processor, and actual cooling requirements depend on the deployed configuration.
For these systems, a cold plate must manage high heat flux while maintaining low thermal resistance, a suitable contact surface, reliable coolant channels, and leak-resistant joints. Flatness and interface conformity affect contact quality, while channel design must balance heat transfer against pressure drop. Manufacturing tolerances and post-joining machining are important because small deviations at the thermal interface can influence performance across a large installed fleet.
Jindu supports cold plate manufacturing through precision CNC machining, with stated tolerance capabilities of ±0.005 mm or ±0.05 mm where the specific feature, process, and drawing requirements permit. These values should not be interpreted as a universal tolerance for every surface or component. Our 100% air-tightness testing provides a final verification step for coolant-boundary integrity. Explore our liquid cold plate solutions for data center cooling.
EV Battery Thermal Management
In electric vehicle battery thermal management, the objective is not simply to make the battery as cold as possible. Consistent temperature distribution across cells and modules is essential because temperature differences can affect performance, charging behavior, aging, and system control. Cold plate channel layouts, contact conditions, coolant distribution, and the thermal interface between the plate and battery assembly all contribute to temperature uniformity.
Serpentine channels and other routed passage geometries are common ways to distribute coolant across a defined footprint. Their suitability depends on the required flow distribution, allowable pressure drop, packaging constraints, and thermal load. The design must also account for joining reliability and the mechanical conditions experienced during vehicle operation.
Jindu can support channel-layout development, joining-process selection, and sealing requirements for cold plate assemblies. For programs requiring production consistency, IATF 16949 quality-system capability is relevant to the transition from prototype evaluation to repeatable manufacturing, subject to the applicable certification scope and project requirements.
IGBT and Power Electronics
IGBT modules and other power electronics generate concentrated heat that must be removed within strict component temperature limits. One of the central design trade-offs is thermal resistance versus pressure drop. Narrow passages, dense fins, pin-fin structures, and angled features can increase coolant contact area or promote mixing, but these benefits may require additional pumping power. The best geometry is therefore the one that meets the thermal target while remaining within the system’s available flow and pressure budget.
Pin-fin and oblique-fin geometries have been reported to reduce thermal resistance by approximately 46–60% in particular comparisons, but this range is not a universal improvement factor. Results depend on the baseline design, fin dimensions, coolant properties, flow rate, and measurement conditions; pressure drop may increase as well. Performance claims should be validated against a clearly defined reference configuration.
Jindu’s manufacturing options include pin-fin and skived-fin structures, together with FSW and vacuum brazing for appropriate cover-sealing designs. Selection should be based on the target thermal resistance, permitted pressure drop, material, operating pressure, and dimensional requirements rather than on fin geometry alone.
Fiber Laser and Medical / High-Power Equipment
Fiber laser systems and other high-power equipment can require precise temperature control because temperature differences across multiple heat-generating components may affect output stability and overall system performance. In fiber laser assemblies with multiple pump sources, temperature uniformity can be as important as the absolute temperature reached at a single point. Some designs target temperature variation of ±2°C or tighter, although the appropriate limit depends on the equipment architecture and the manufacturer’s requirements.
These applications may require carefully routed coolant channels, stable thermal interfaces, predictable flow distribution, and tight control of the finished contact surface. The plate must also maintain coolant-boundary integrity throughout its specified operating conditions. Thermal analysis helps evaluate whether the proposed channel geometry can provide the required temperature distribution without exceeding the available pressure drop.
Jindu supports precision channel machining, thermal simulation, heat-dissipation analysis, and air-tightness validation as part of cold plate development — including channel layouts that support the temperature uniformity targets described above. For laser-specific applications, see our laser cooling liquid cold plate page.
How to Specify a Cold Plate: A Practical Checklist for Engineers and Buyers
A useful cold plate specification connects thermal requirements to mechanical interfaces, hydraulic limits, manufacturing processes, and quality-control criteria. The following checklist helps engineering teams and buyers define the requirements before requesting quotations or approving a production drawing.
-
Heat Load and Heat Flux
Define the total heat load and, where possible, the heat distribution over the contact area. Total heat load helps establish the amount of energy the coolant must carry away, while heat flux indicates how concentrated the thermal input is. These values influence base thickness, fin density, channel placement, and the required contact area. Jindu can use the supplied heat-load conditions and mechanical constraints as inputs for cold plate geometry and manufacturing discussions.
-
Allowed Thermal Resistance
Specify the maximum permitted thermal resistance or the required component temperature under defined operating conditions. This requirement helps determine material selection, base geometry, channel architecture, and the extent of heat-transfer surface area needed. The target should be evaluated together with coolant inlet temperature, flow rate, heat load, and interface conditions. Jindu can support thermal simulation and heat-dissipation analysis to help evaluate a proposed design against its intended requirements.
-
Pressure Drop Budget
Define the allowable pressure drop across the cold plate at the intended coolant flow rate. Channel width, channel height, pin-fin spacing, passage length, and flow distribution all influence hydraulic resistance. A design may achieve the desired thermal performance at one flow rate but become unsuitable if the pump cannot provide the required pressure. Jindu can review channel geometry and manufacturing feasibility alongside the specified hydraulic limits so that thermal targets are not considered in isolation.
-
Coolant and Loop Material
Identify the coolant formulation, operating temperature range, expected flow conditions, wetted materials, and any required corrosion inhibitors. Copper, aluminum, stainless steel, coatings, seals, and fittings must be evaluated as part of the same loop. A coolant that is suitable for one material combination may not be appropriate for another. Review the coolant compatibility section and confirm the selected chemistry with the coolant supplier. Jindu can assess material and manufacturing-process options in relation to the defined operating environment.
-
Flatness, Conformity, and Mounting Pressure
Specify the contact-surface geometry, relevant datums, mounting method, clamping force, and TIM requirements. A perfectly flat cold plate may underperform on an AMD platform whose IHS carries a slight curvature; conformity to the target IHS profile can matter more than absolute flatness. Specify the interface, not just the plate. The required surface geometry should be based on the actual component package and mounting conditions rather than an assumption that every mating surface should be perfectly planar.
Flatness must also remain sufficiently stable over the intended thermal and mechanical duty cycle. A plate that meets its initial tolerance but changes shape under repeated heating and cooling may accelerate TIM pump-out and degrade contact over time. The specification should distinguish initial flatness from the required dimensional stability after relevant processing and operating conditions. Jindu’s stated CNC tolerance capabilities include ±0.005 mm and ±0.05 mm for applicable features; the achievable tolerance and inspection method must be confirmed against the drawing, material, and process route.
-
Leak Integrity Requirement
Specify the coolant boundary, operating pressure, test method, acceptance criteria, and any required test documentation. The sealing method may influence the choice between FSW, vacuum brazing, soldering, or another suitable joining approach. Test conditions must be appropriate to the design and the customer’s acceptance requirements. Jindu performs 100% air-tightness testing before shipment, making final leak verification a defined part of the manufacturing and quality-control process rather than an assumption based only on the joining method.
-
Drawing CTQs
Identify the critical-to-quality characteristics directly on the drawing or in the accompanying specification. Datums must correspond to the actual clamping and measurement references; sealing surfaces should include appropriate surface-roughness requirements; channels should have defined cleanliness, flushing, and drying requirements; and post-joining flatness requirements should allow for finish machining after the joining process. Most cold plate failures are not thermal-math problems — they come from CTQs that were never defined on the drawing.
Manufacturing requirements should also state which dimensions are critical, how they will be measured, and what constitutes acceptance. If brazing or FSW can distort the contact face, the process plan should define the required machining allowance and the point at which final dimensional inspection and leak testing occur. Jindu can review drawing requirements to identify manufacturing considerations before the design enters production.
-
Prototype-to-Production Path
Define the expected prototype quantity, sample turnaround requirements, production volumes, inspection requirements, and anticipated demand changes. A prototype that demonstrates thermal performance is not automatically proof of stable mass-production capability. Tooling, process controls, material sourcing, cleaning procedures, joining parameters, and final inspection must be suitable for the intended production volume. Jindu supports development from prototyping to mass production, with stated annual part capacity above 50,000 units and IATF 16949 quality-system capability, subject to the applicable product and certification scope.
Once these requirements are documented, engineering teams can compare manufacturing proposals on a consistent basis. To discuss drawings, operating conditions, or production requirements, request a quote or contact the engineering team.
Why Jindu: Manufacturing Depth Behind the Cold Plate
Jindu combines skiving, friction stir welding, vacuum brazing, soldering, and precision CNC machining to support mainstream cold plate architectures, from tubed designs to skived-fin and brazed assemblies. The manufacturing route is selected according to the required channel structure, thermal interface, sealing method, and dimensional requirements.
Our stated quality capabilities include 100% air-tightness testing before shipment, with thermal simulation and heat-dissipation analysis support for appropriate projects. IATF 16949 quality-system capability supports the transition from prototype development toward production programs, subject to the applicable certification scope and customer requirements.
If you are developing a cold plate for electronics, power systems, data centers, or other demanding thermal applications, start with the component’s heat load, coolant conditions, interface drawing, and pressure requirements. Visit our liquid cold plate manufacturing page or contact our engineering team to discuss your design and request a quote.
Frequently Asked Questions
Cold Plate vs. Heat Sink — What’s the Difference?
A conventional heat sink transfers heat into the surrounding air, usually through fins and natural or forced airflow. A liquid cold plate transfers heat into a coolant flowing through internal passages, which carries the energy to a remote heat exchanger. A cold plate can be advantageous when heat flux is high, space is limited, or the system needs controlled heat removal. The best choice depends on the thermal load, operating environment, available airflow, and overall system design.
How Much Pressure Drop Is Acceptable for a Cold Plate?
There is no single acceptable pressure-drop value for every cold plate. The limit depends on the available pump head, required flow rate, the pressure losses of the rest of the loop, and the thermal performance target. A cold plate with dense fins or narrow passages may improve heat transfer while increasing hydraulic resistance. Specify pressure drop at a defined coolant, temperature, and flow rate, then evaluate the result alongside the complete system’s pumping capacity.
Can a Cold Plate Be Repaired After a Leak?
Repair feasibility depends on the leak location, base material, joining method, coolant contamination, operating pressure, and required reliability. Some external fittings or accessible joints may be serviceable, while a leak through an internal passage or a sealed brazed or welded assembly may require replacement. Any proposed repair must be assessed for material compatibility, structural integrity, dimensional changes, and repeat leak-test results. This is also why the joining method and post-join machining sequence described in the FSW and vacuum brazed sections matter for serviceability. For safety-critical or high-reliability applications, replacement may be more appropriate than an unqualified repair.
Is Copper Always Better Than Aluminum for Cold Plates?
No. Copper generally offers higher thermal conductivity, but it is heavier and may have higher material and manufacturing costs. Aluminum provides a useful balance of weight, thermal performance, machinability, and compatibility with manufacturing processes such as skiving and FSW. The best choice depends on heat flux, allowable thermal resistance, coolant chemistry, joining requirements, and cost. Material selection should be made together with the channel architecture and manufacturing process.
What Filtration Level Does a Microchannel Cold Plate Need?
The required filtration level depends on the smallest channel feature, particle contamination risk, coolant condition, and allowable pressure drop across the filter. A 25–50 μm filter rating may be an initial reference for some microchannel systems, but it should not be applied universally. The specification should account for particle size and shape, filter capacity, and the possibility of contamination introduced during manufacturing or maintenance. Channel cleanliness, flushing, drying, and verification are also necessary because filtration alone cannot remove residues already trapped inside a plate.
How Is a Cold Plate Leak-Tested?
Cold plates may be checked using a suitable pressure-decay, pressure-hold, or tracer-gas method, depending on the design, sensitivity requirement, and acceptance specification. The test pressure, duration, medium, and allowable leakage must be defined for the application. Testing should take place after final machining and any operation that could affect the coolant boundary. Jindu performs 100% air-tightness testing before shipment according to applicable product requirements; the specific method and acceptance criteria should be confirmed for each project.

